· 2 min read
AI Vision & Supply Chain Automation.
AI and computer vision are transforming supply chain management — enabling autonomous monitoring, real-time quality control, predictive maintenance, and end-to-end traceability across procurement, production, warehousing, and distribution.
AI across the supply chain
The supply chain is a sequence of interdependent processes — and AI creates value at every stage. By combining computer vision with IoT sensors and autonomous decision-making, manufacturers gain real-time visibility and control from raw material intake to final product delivery.
- 01
Procurement
Incoming inspection & supplier QC
- 02
Production
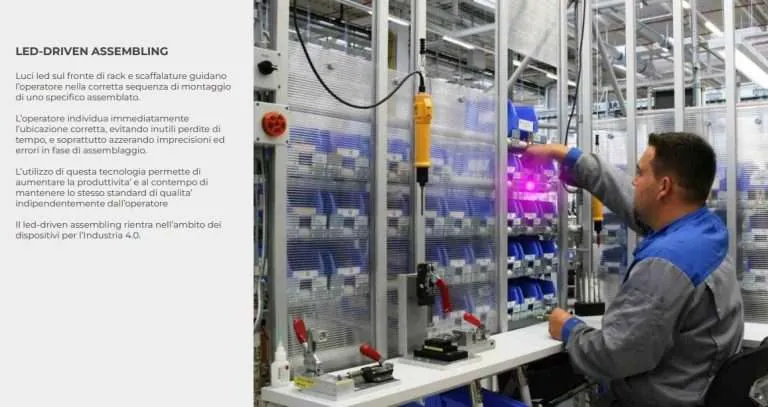
Defect detection & assembly verification
- 03
Warehousing
Inventory counting & picking verification
- 04
Distribution
Packaging QC & shipment traceability
What AI vision systems do in the supply chain
Integrated with IoT sensors and production systems, AI vision platforms act autonomously — observing, deciding, and acting without waiting for human intervention.
- 01
Autonomous quality monitoring
Continuously inspects goods and production processes — detecting defects, anomalies, and non-conformances in real time at every stage of the supply chain.
- 02
Dynamic decision optimisation
Adapts automatically to demand variations, resource availability, and production priorities — rerouting flows and adjusting schedules without manual intervention.
- 03
End-to-end synchronisation
Connects and synchronises every supply chain node — procurement, production, warehousing, and distribution — with shared real-time data and automated triggers.
- 04
Predictive maintenance
IoT vibration and vision sensors detect early signs of equipment failure — scheduling maintenance before breakdowns disrupt production schedules.
- 05
Inventory and stock optimisation
Computer vision counts and tracks stock automatically — providing accurate, real-time inventory levels without manual scanning or periodic counts.
Industry applications
AI supply chain solutions adapt to the specific requirements of each sector — from food safety compliance to pharmaceutical precision to electronics tolerances.
- 01
Food & Beverage
Hygiene monitoring, contamination detection, grading and sorting, traceability from farm to shelf — HACCP and food safety compliance built in.
- 02
Pharmaceutical
High-precision inspection of vials, ampoules, and packaging — GMP compliance, batch traceability, and regulatory documentation automated.
- 03
Electronics
PCB defect detection, micro-component verification, and ultra-tight tolerance inspection — at the speed and consistency that manual inspection cannot achieve.
Benefits of AI-driven supply chain automation
Reduced inspection errors and handling mistakes across all supply chain stages
Better management of demand peaks and urgent orders without adding headcount
Higher productivity through autonomous process execution and fewer manual interventions
End-to-end visibility and traceability — full digital record of every product movement
Dynamic stock optimisation — accurate real-time inventory without manual counting
Self-learning systems — performance improves continuously with every production run
- 01
Key capabilities
Inspection 100% inline Processing Edge / Cloud Integration ERP / MES / IoT Sectors 10+ Deploy 1 day
- 02
Related guides
Smart factory guide Connected machines & OEE Pick to Light + AI
Related reading
More guides on AI, automation, and smart manufacturing.
Guide · Industry 4.0 Smart Factories, AI & Computer Vision Read more
Guide · Industry 4.0 Connected Machines, AI & OEE Read more
Guide · Logistics Pick to Light + Vision + AI Read more